High-Density Engineered Technical Socks (Part I)
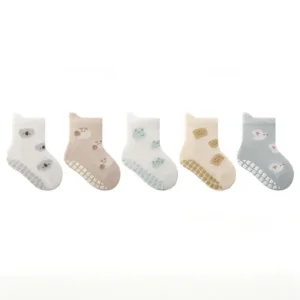
Verified production line outputs combining anti-slip grip silicones, moisture-wicking capillary yarns, and reinforced biomechanical stress zones.
Macro Dynamics in Mens Sports Socks Sourcing & Procurement
The global sports hosiery industry has shifted dramatically from commodity daily apparel into precision-engineered biomechanical hardware. Technical performance wear now dictates customer retention.
Shifting Elastic Demand
Global athleisure and activewear markets demand mens athletic socks that transition effortlessly from high-impact sports (soccer, basketball, cross-training) to casual executive wear. Premium consumers demand targeted arch support, graduated compression (15–20 mmHg), and non-slip sole anchors without compromising visual sophistication.
Performance Friction Engineering
Repetitive blister injuries and energy dissipation inside athletic footwear have made grip-pad silicone formulations an imperative standard. Modern sports programs require thermoplastic polyurethane (TPU) and food-grade silicone grip arrays on soles to eliminate inner-shoe slippage and maximize kinematic torque transfer.
Direct-to-Consumer Pressure
E-commerce and specialty subscription sock brands have compressed retail turnaround cycles. B2B importers, Amazon brand operators, and retail buyers no longer tolerate 120-day production backlogs, requiring nimble high-speed suppliers that offer flexible low-MOQs with rapid pre-production digital physical-proof turnarounds.
Localized End-Use Scenarios: Engineering for Specific Athletic Disciplines
A single universal sock specification fails under intense field stress. Our factory configures needle count, yarn composition, and terry looping based on strict kinematic criteria.
Field Sports: Football & Rugby
Soccer players endure high angular sheer. Our men's football grip socks incorporate hexagonally molded silicone nubs on the plantar surface to lock the foot to the insole, while 168-needle double-cylinder construction prevents cuff slipping during explosive deceleration and directional pivot turns.
Court Athletics: Basketball & Padel
Hardwood and synthetic courts inflict severe vertical impact. Engineered with high-density terry loop cushioning across the calcaneus (heel) and metatarsal pads, these socks cushion landings while breathable mesh instep channels evacuate vapor to mitigate athlete blister formation.
Endurance: Marathon, Trail & Cycling
Long-duration running exposes fibers to saturated moisture. We blend polyamide with hydrophobic functional yarns, employing a hand-linked seamless toe closure (Rosso/Hand link) to prevent micro-abrasions, coupled with a targeted 360-degree arch compression strap that reduces plantar fatigue.
| Discipline | Needle Count & Machine | Recommended Yarn Blend | Grip & Cushioning Technology | Key Performance KPI |
|---|---|---|---|---|
| Football / Soccer Grip | 168N / Single or Double Cylinder | 75% Combed Cotton, 20% Nylon, 5% Spandex | Plantar silicone chevrons, ankle brace ribbed wrap | Zero in-shoe slip during 90-min shear tests |
| Court / Basketball | 144N / Thick Terry Specialized | 80% Cotton, 15% Polyester, 5% Elastane | Triple-density French terry sole, Achilles cushion tab | 35% impact dampening at heel strike |
| Marathon / Running | 200N / High-Gauge Precision | 50% CoolMax/Dryarn, 45% Nylon, 5% Lycra | Ultralight thin sole, localized zonal mesh window | Sub-20 minute evaporative drying index |
| Outdoor Hiking / Trail | 132N / Heavy Gauge Thermal | 65% Merino Wool, 25% Polyamide, 10% Elastic | Full-foot dense looped terry, reinforced toe & heel cap | Thermal insulation (R-value > 0.45) wet or dry |
China Factory Ecosystem: Supply Chain Resilience & Scaling Kinetics
Why Tier-1 international apparel brands entrust mission-critical wholesale sports socks manufacturing to our automated Sichuan manufacturing hub.
Raw Material Cluster Integration
Our proximity to domestic fine-staple combed cotton producers, high-tenacity nylon extruders, and certified Oeko-Tex dye facilities isolates our supply chain from global yarn stock bottlenecks, guaranteeing raw material cost predictability even amid fluctuating commodity markets.
Vertically Unified 42,000m² Campus
Founded in 2013, Sichuan MiFo Technology Co., Ltd. eliminates subcontractor margins and cross-factory shipment delays. From technical vector digitizing to computerized knitting, automated silicone vulcanization, pressure setting, and custom barcoded packaging—all processes are fully enclosed.
Reliability SLA (99.4% Delivery)
With an annual factory volume eclipsing 200 million pairs, our operational cadence accommodates both steady multi-container seasonal replenishments and rapid 15-day expedited contract runs without cannibalizing production lead times or compromising rigorous QC.
Technical Roadmap: Next-Generation Mens Athletic Hosiery
The convergence of functional biochemical additives, recycled polymer circularity, and smart-wear biometric interfaces.
Permanent Antimicrobial Yarn Infusion
Moving away from topical wash coatings that deplete after 15 launders, our engineering lab integrates zinc pyrithione, silver ions, and copper nano-particles directly into the core polymer melt before spinning, guaranteeing 99.9% anti-odor efficacy through 50+ industrial washes.
Circular Economy & Recycled Polymers
Complying with ESG corporate mandates, we utilize GRS-certified (Global Recycled Standard) rPET poly yarns derived from post-consumer ocean plastics, blended with traceable organic cottons dyed using zero-discharge waterless tinting techniques.
Biometric & Conductive Smart Knits
Collaborating with sports science institutions, we are prototyping conductive carbon-threaded socks capable of transmitting continuous pressure-point metrics, stride cadence, and foot strike distribution directly to sports telemetry devices.
Global Market Localization & Regulatory Compliance
Cross-border importing demands airtight compliance. We de-risk international procurement with institutional third-party audit credentials and localized regulatory adherence.
Social & Ethical Factory Audits
Our production facilities maintain active, top-tier audits under BSCI (Business Social Compliance Initiative) and Sedex SMETA standards, ensuring zero labor violations, safe workplace governance, and seamless verification for major global department stores.
Chemical & Environmental Safety
Every batch of sport socks conforms strictly with EU REACH Annex XVII, US CPSIA, and OEKO-TEX Standard 100 Class I/II specifications. Our products are laboratory certified free of AZO dyes, formaldehyde, phthalates, organotins, and extractable heavy metals.
Customs Tariff & Packaging Optimization
We provide full documentation (GSP Form A, RCEP Certificates of Origin, EUR.1) to lower tariff burdens. Packaging solutions include multilingual retail cards, FSC-certified hangtags, anti-theft RFID microchips, and polybags pre-labeled for Amazon FBA fulfillment centers.
High-Density Engineered Technical Socks (Part II)
Explore customized configurations, high-stretch elastic cuffs, and anti-slip silicone applications tailored for wholesale buyers worldwide.
Frequently Asked Questions: Technical Sourcing & Factory Verification
In-depth responses compiled by senior hosiery engineers and international export trade officers.
What differentiates athletic mens sports socks from standard commodity crew socks?
Mens sports socks feature high-needle density engineering (144N, 168N, or 200N), zonal cushioning, targeted elastane tension bands, and specific functional fiber choices. Unlike everyday casual socks made of uncombed carded cotton, performance athletic socks utilize high-count combed cotton, moisture-channeling polyamides, and localized terry-loop padding to damp impact and prevent chafing blisters under severe friction.
What are your Minimum Order Quantities (MOQs) for custom-branded mens sports socks?
Our standard MOQ is typically 1,000 pairs per design/colorway for fully custom jacquard, grip printing, and private-label packaging programs. For specialized yarn requests (such as GRS-certified recycled polymers, CoolMax, or Merino wool blends), MOQs can vary between 1,500 to 3,000 pairs depending on the minimum dye lot constraints of the raw spinning mills.
How does Sichuan MiFo ensure silicone non-slip grip durability through repetitive washing cycles?
We deploy high-temperature automated vulcanization and liquid silicone injection systems rather than basic PVC plastisol transfers. Our medical-grade silicone formulas achieve deep mechanical interlocking within the yarn fibers, passing standardized 50-cycle commercial laundering and dry friction tests without peeling, crumbling, or loss of adhesion coefficient.
What quality control mechanisms are implemented during bulk sports sock manufacturing?
Our factory employs a strict 4-stage Quality Inspection protocol: (1) Inbound yarn tensile and colorfastness inspection; (2) In-line gray sock knitting monitoring for skipped stitches or loop irregularities; (3) Post-linking manual toe seam stress checks; and (4) Final needle-detector scanning and pre-shipment AQL 2.5/4.0 standard carton audits.
Can MiFo manage rapid sample prototyping and drop-shipping of pre-production samples?
Yes. Upon receipt of vector artwork files (AI, PDF, or CAD), our pattern division converts designs into knitting machine program files within 24 hours. Physical counter-samples are typically knitted, vulcanized, finished, and dispatched via international air courier within 5 to 7 business days for buyer sign-off.
Which international regulatory standards do your manufacturing operations satisfy?
Our facilities are audited under BSCI and Sedex SMETA social responsibility standards. Finished goods meet OEKO-TEX Standard 100, REACH Annex XVII, CPSIA, and California Proposition 65 requirements, ensuring all athletic socks are free from hazardous phthalates, organotins, formaldehyde, and heavy metals.