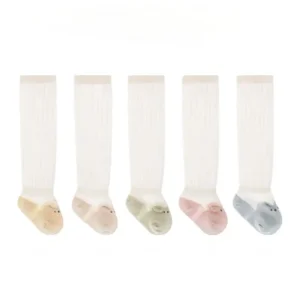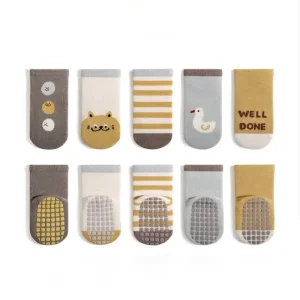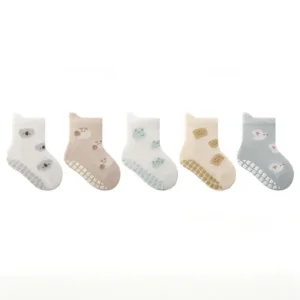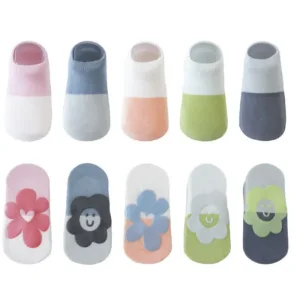
Certified Flight & Performance Core Product Line
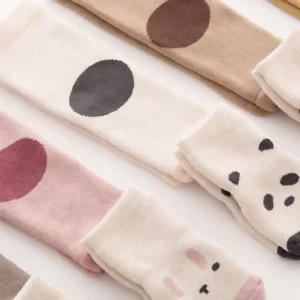
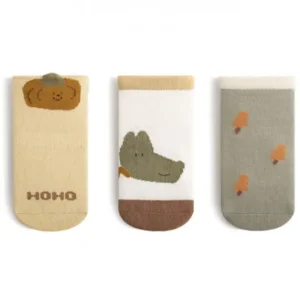
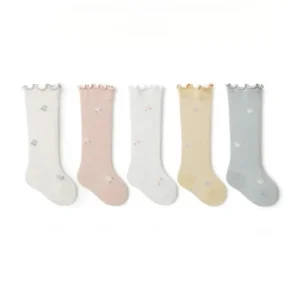
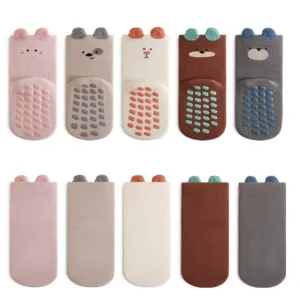
Explore initial selections from our vertically integrated automated hosiery facility. Retaining proprietary ergonomics, non-slip precision, and advanced comfort architectures.
Aeromedical Engineering: The Physiology of In-Flight Circulation
Prolonged immobility inside pressurized aircraft cabins (typically 6,000–8,000 ft barometric equivalents) severely impacts venous blood velocity in the lower extremities, exacerbating pooling and elevating Deep Vein Thrombosis (DVT) probability.
Venous Return Acceleration
Long-haul flights drop calf muscle pump activity to near zero. True graduated compression counters hydrostatic pressure by applying 100% target pressure at the ankle, scaling to 70% mid-calf and 40% near the popliteal fossa to keep blood flow elevated.
- Enhances femoral vein flow by up to 38%
- Reduces microvascular interstitial fluid leakage
- Minimizes peripheral edema during 8+ hour flights
DVT & Economy Class Syndrome
Cabin air hypobaric hypoxia alongside dry conditions (often <15% humidity) increases blood viscosity. Graduated elastic hosiery counteracts stasis—the primary pillar of Virchow's triad—preventing micro-thrombi formation in vulnerable travelers.
- Clinically recognized prophylaxis for travelers
- Suppresses deep vein valve distension
- Balances internal muscular venous pressure
Standard vs Flight Socks
Standard athletic or daily socks apply non-calibrated uniform pressure that can form a tourniquet ring around the upper calf, worsening venous pooling. Certified travel compression socks use computer-controlled inlaid elastane loops for true graduation.
- Zero constriction bands at popliteal fold
- Calibrated millimetric degressive curve
- Non-binding wide welt top band construction
China Factory 4.0: Supply Chain Resilience & Modern Production
At our integrated 42,000 m² Sichuan production facility, Sichuan MiFo Technology Co., Ltd. combines advanced computerized hosiery engineering with automated quality validation to deliver stable bulk export programs.
Lonati Automated Knitting
High-precision 144N, 168N, and 200N computerized cylinders integrate positive feeder systems to control elastane tension with millimetric accuracy.
Salzmann Testing
Every batch undergoes MST IV / Salzmann pressure profilometry across ankle (B), calf (C), and under-knee (D) points to ensure strict international compliance.
Real-time MES Tracking
Digital production monitoring links raw yarn intake through knitting, Rosso toe closing, boarding, and silicone application for transparent lot traceability.
Raw Material Advantage
Direct volume sourcing of Invista Lycra, combed cotton, and technical nylon delivers medical-grade performance with balanced OEM production costs.
Graduated Pressure Profiles & Technical Roadmaps
Meeting medical class expectations and commercial traveler comfort standards through strict adherence to CEN, British Standard, and RAL-GZ 387 frameworks.
| Compression Class | Pressure Level (Ankle B) | Target Demographic / Use Case | Recommended Yarn Structure | Compliance Framework |
|---|---|---|---|---|
| Class I (Mild) | 15–20 mmHg | Frequent flyers, airline cabin crew, casual business travel, early edema prevention | Combed Cotton (65%), Nylon (25%), Lycra Spandex (10%) | BS 6612, FDA Class I, OEKO-TEX Standard 100 |
| Class II (Moderate) | 20–30 mmHg | Long-haul routes (>8 hrs), pre-existing varicose veins, DVT prevention, post-sclerotherapy | Microfiber Nylon (72%), Double-Covered Spandex (28%) | RAL-GZ 387/1, CE MDR Class I, ISO 13485 |
| Class III (Firm/Medical) | 30–40 mmHg | Severe chronic venous insufficiency, post-thrombotic syndrome, clinically directed travelers | High-denier Polyamide (70%), Specialized Core-Spun Elastane (30%) | Medical Device Directive (EU) 2017/745, RAL Class III |
| Recovery / Hybrid Travel | 18–22 mmHg | Athletes traveling to overseas competitions, mixed transit and dynamic movement | Coolmax/Dryarn (50%), Nylon (35%), Spandex (15%) with targeted terry sole | SATRA TM434, ISO 9001 certified batch controls |
Enterprise Procurement Needs: Private Label, Airlines & Pharmacies
Custom-tailored supply chain architectures addressing the distinct requirements of multinational retailers, corporate travel health providers, and institutional buyers.
Direct-to-Consumer & Retail Brands
For fashion-forward travel wellness brands needing refined aesthetics without compromising certified compression metrics.
- 360° seamless digital printing and multi-color jacquard
- Retail-ready packaging: FSC-certified hangtags, soft-touch matte boxes
- Flexible MOQs for seasonal capsule collections
- Custom yarn blends including organic cotton and bamboo viscose
Airlines & Travel Amenities
Providing long-haul business/first-class passenger kits and uniform hosiery for cabin crews and pilot associations globally.
- Cost-effective high-volume batch runs with lightweight packaging
- Corporate color matching via pantone yarn dyeing
- Anti-odor silver ion finishes for fresh 14+ hour transit
- Custom branding on soles via silicone or woven jacquard tabs
Pharmacy Chains & Medical Suppliers
Strict documentation, batch verification, and consistent sizing systems tailored for over-the-counter medical distribution.
- Strict Salzmann pressure-curve certificates included per shipment
- Full traceability from raw polymer through finished product
- FDA, CE MDR, and OEKO-TEX Standard 100 verification
- Tamper-evident medical packaging with multilingual instructions
Future Innovations, Localization & Global Compliance
Combining sustainable textile chemistry, connected health technologies, and dependable cross-border logistics to deliver forward-looking hosiery manufacturing.
Cross-Border Compliance
Our facilities maintain active social compliance and quality certifications including BSCI, Sedex SMETA, ISO 9001, and medical device standards. We deliver complete documentation packets for rapid customs clearance across North American, European, and Asia-Pacific ports.
Eco-Circular Materials
Transitioning toward closed-loop circular systems: wholesale partners can specify GRS-certified recycled nylon, bio-based spandex, and post-consumer regenerated polyester fibers without compromising elasticity retention or compression tolerances.
Smart Sensory Integration
In pilot R&D with technical university partners: integrating conductive elastomer sensor threads capable of monitoring calf circumference changes and venous pressure differentials in real-time, designed for future commercial flight applications.
Frequently Asked Sourcing & Technical Questions
Addressing essential questions from international procurement directors, technical designers, and medical supply chain officers.
What is the standard MOQ for custom flight compression socks?
Our standard MOQ is 1,000 pairs per design/colorway for fully custom-knitted graduated styles. For plain base colors utilizing custom silicone grips, branded embroidery, or customized packaging, MOQs can be negotiated from 500 pairs per size run.
How do you verify true graduated compression throughout production?
We utilize Swiss-engineered Salzmann MST IV testing units. During production runs, randomized inline samples are checked across points B (ankle), B1 (Achilles), C (calf calf girth), and D (below knee) to ensure the pressure gradient matches targeted medical-grade curves.
Can you provide custom sizing specifically designed for western demographics?
Yes. We have developed specialized size matrices specifically suited for North American and European traveler demographics, accommodating wider calf circumferences (wide-calf sizes up to 24 inches) while keeping ankle compression strictly calibrated.
What certifications and ethical audits does your factory maintain?
Our manufacturing base operates under BSCI and Sedex SMETA social responsibility audits. In terms of materials and medical quality assurance, our output complies with OEKO-TEX Standard 100, CE MDR, and FDA requirements for Class I devices.
What is the typical sampling and bulk production lead time?
Digital technical proofs are delivered within 48 hours. Physical counter-samples take 7–10 days. Once pre-production samples are approved, bulk manufacturing for 10,000–50,000 pairs is completed within 25–35 days, supported by expedited sea/air freight booking.
Can you incorporate anti-slip soles without compromising compression?
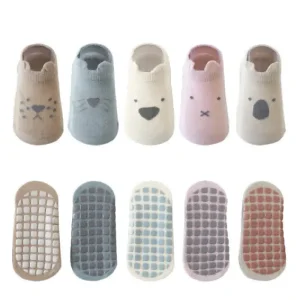
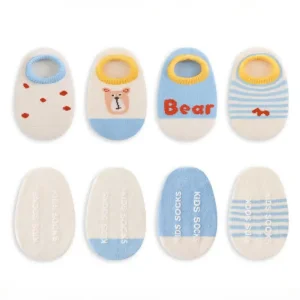
Yes. As a leading manufacturer of functional non-slip socks, our screen and rotary silicone printing processes apply high-friction silicone pads to the sole bed without affecting the longitudinal elasticity of the calf shaft.
Functional, Anti-Slip & Extended Hosiery Portfolio
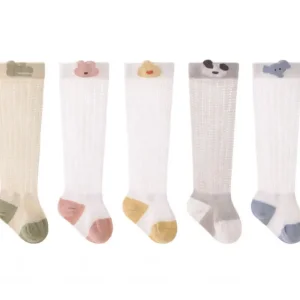
Complete product spectrum manufactured at our 42,000 m² Sichuan base, covering functional grips, breathable constructions, and high-durability knitted solutions.