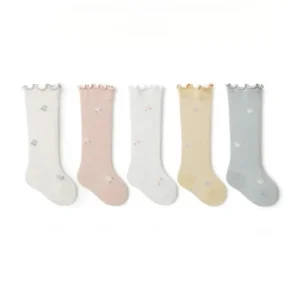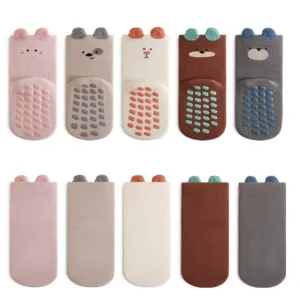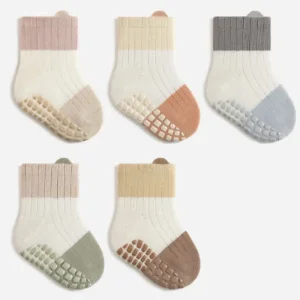
Featured Bulk & Disposable Hosiery Lines
Direct-from-factory inventory optimized for institutional replenishment, clinical grade compliance, and rapid consumer wear.
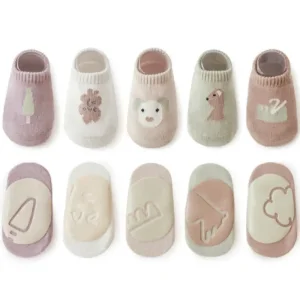
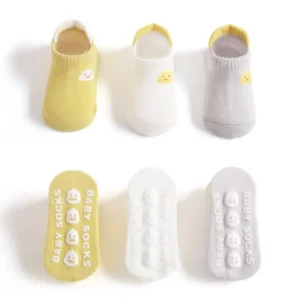
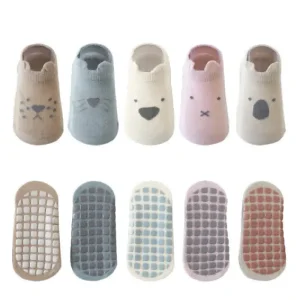
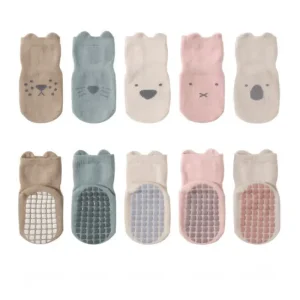
Over a decade of advanced high-volume hosiery engineering.
Automated computerized cleanrooms & packing hubs.
Pairs supplied annually across tier-1 international supply chains.
Global fulfillment hubs supporting EU, US, and APAC markets.
Global Demand Vectors for Travel Disposable Socks
Institutional buyers require reliable microbial barrier defense, lightweight logistics compression, and non-toxic skin-contact certifications to meet strict multi-regional regulations.
Aviation & Cruise Travel Kits
Long-haul airline cabins and luxury cruise operators require ultra-soft, lint-free single-use socks designed for pressure redistribution, thermal retention, and premium passenger touchpoints during transit.
Hospitality, Spas & Wellness
Five-star hotels, luxury thermal bath resorts, and aesthetic clinics deploy disposable hygienic foot barriers that preserve clean-floor protocols while delivering luxurious skin feel and breathable micro-mesh comfort.
High-Throughput Try-On & Retail
Shoe retailers, bowling alleys, and sports apparel flagships eliminate cross-contamination risks by providing economical, sanitary single-use foot covers packed for fast, low-friction dispenser distribution.
Industrial Sourcing & Compliance Verification
Sichuan MiFo Technology Co., Ltd. combines computerized circular knitting arrays with multi-tier optical and tensile inspection to secure unmatched batch-to-batch integrity.
BSCI & Sedex Audits
Strict adherence to ethical employment, safe labor criteria, transparent trace loops, and environmentally responsible manufacturing standards verified by third-party inspectors.
99.4% On-Time Record
Fully integrated yarn-to-shipment logistics keep mega-orders protected against bottlenecks, guaranteeing high dispatch consistency across major sea and air freight lanes.
OEKO-TEX Standard 100
Zero hazardous chemicals, heavy metals, or carcinogenic AZO dyes. Suitable for hypersensitive dermatological applications, clinical cleanrooms, and long journeys.
Custom Packaging Arrays
From vacuum-sealed compression travel packs and retail blister packaging to bulk cardboard dispensing systems customized with custom UPC codes and branding.
Technical Specification Matrix: Travel & Functional Socks
Direct comparative benchmarks to help brand managers and supply chain directors choose the right knit count, yarn blend, and finishing process.
| Application Vector | Core Composition | Knitting Machine Gauge | Key Functional Highlights | Primary Commercial Clients |
|---|---|---|---|---|
| Aviation & Travel Disposable | 100% Micro-Poly / Spandex core | 144N – 168N single cylinder | Ultra-lightweight, skin-friendly, compact volume | Airlines, railway operators, tour suppliers |
| Sanitary & Footwear Try-On | Virgin Spunbound / Poly blend | 96N – 120N high-speed weave | Cost-effective, barrier hygiene, elastic closure | Shoe retail chains, bowling lanes, museums |
| Medical & Fall-Prevention Slipper | Cotton-Poly core + dual silicone dots | 108N – 144N terry cushion | High-traction silicone grip, non-constricting cuff | Hospitals, elderly care centers, clinics |
| Indoor Parks & Trampolines | Combed Cotton / High Elastic Spandex | 144N reinforced heel & toe | Customized high-friction tread, tear-resistant structure | Trampoline parks, family entertainment hubs |
| Aqua Park & Watersport Hosiery | Hydrophobic Nylon / Neoprene yarn | 168N double-needle seamless | Quick-drying, thermal shielding, wet slip-resistance | Water parks, dive resorts, wellness spas |
R&D Roadmap: Sustainable & Smart Single-Use Hosiery
Our engineering facility is actively modernizing disposable textile lifecycles through zero-waste circularity and bio-compatible polymer integration.
Biodegradable PLA Fibers
Integrating Polylactic Acid (PLA) synthesized from renewable corn starch. Achieves 100% industrial compostability within 180 days, reducing enterprise carbon footprint across hospitality clients.
Clean Waterless Dope-Dyeing
Deploying pre-extrusion yarn pigment infusion to eliminate toxic liquid effluent, saving over 80% water and 60% energy compared to traditional piece-dye methods.
Micro-Encapsulated Bio-Agents
Embedding natural tea polyphenols and silver-ion microcapsules directly into disposable fibers to neutralize bacterial odors during long flights and cruise stays.
AI Robotic Vision QA
High-speed optical visual inspection cameras integrated into each automated linking unit, detecting microscopic stitch gaps and ensuring zero-defect carton packaging.
Frequently Asked Sourcing Questions
Practical technical answers from our international engineering and trade compliance desk.
For stock white or plain black disposable knits, MOQs start as low as 1,000 to 3,000 pairs. For fully customized yarn compositions, Pantone color matching, jacquard brand logos, or specialized anti-slip silicone tread patterns, our production run starts at 5,000 to 10,000 pairs per design.
Yes. We provide automated heat-sealed single-pair OPP/PE barrier packaging, cleanroom inner poly-lining, and ethylene oxide (EO) sterilization validation support upon client request for healthcare, dental, or clinical cleanroom deployments.
We recommend high-filament micro-polyester intertwined with low-denier elastane, or an ultra-fine combed cotton blend. This achieves strong hygroscopic moisture dispersion while preventing foot compression marks on swelling extremities during prolonged transit.
We handle DDP, CIF, and FOB terms globally with full HS code documentation, REACH / Prop 65 chemical compliance testing, and BSCI social compliance certifications ready for streamlined clearance through European and American customs.
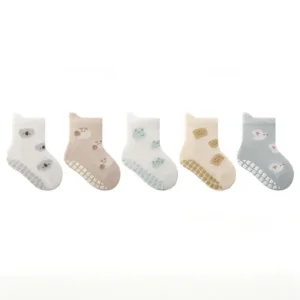
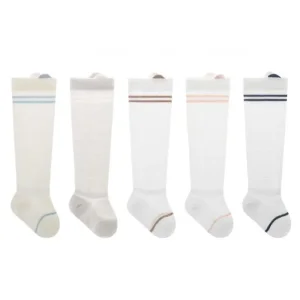
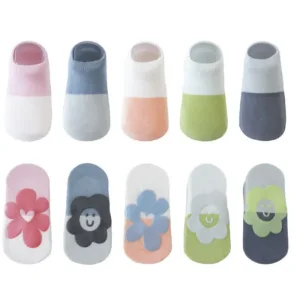
Explore Additional Performance & Infant Hosiery Lines
Engineered for comfort, non-slip grip safety, and durability across multi-category market demands.