Featured Technical Hosiery & Performance Foundations
Discover high-precision knitting architectures, anti-slip innovations, and infant-to-adult engineered garments direct from our integrated manufacturing lines.
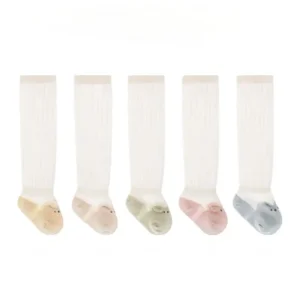
Engineering Alpine Thermal Ergonomics & Industrial Execution
Navigating the high-stakes alpine footwear interface: How high-density needle selections, calibrated shear friction control, and multi-component yarn matrices redefine modern OEM/ODM ski sock manufacturing.
Thermodynamic Balance & Clo Engineering
Ski boot environments impose radical thermal constraints: extreme external sub-zero conditions paired with high microclimatic humidity within impermeable polyurethane boot shells. We utilize micron-graded Australian Merino Wool (17.5-19.5μm) co-knitted with hollow-core synthetic filaments (Thermolite/Primaloft), achieving an optimal Clo insulation rating of 0.35–0.48 without increasing volume or compromising ski boot shell fitment.
Tibial Kinetic Shock Dampening
Alpine touring and carving exert repetitive kinetic shock along the anterior tibial ridge. Our manufacturing deploys 3D variable-density terry loops ranging from 1.5mm to 3.2mm in localized anatomical zones. This architecture reduces localized peak pressure points by up to 34% against rigid ski boot tongues while keeping plantar and lateral profiles razor-thin for zero transmission power loss.
Calibrated Venous Compression
Long alpine descents and high altitudes trigger peripheral venous stasis and calf fatigue. Integrating computerized inverted conical spandex feeds, our factory produces true graduated medical-grade class 1 compression (15-20 mmHg) from supramalleolar points up through the gastrocnemius muscle belly, promoting microvascular return, preventing swelling, and accelerating lactic acid dispersion.
Over a decade of vertically integrated technical hosiery innovation & global export execution.
Consolidated clean automated production lines, testing laboratories, and automated warehousing in Sichuan, China.
Mass-scale manufacturing bandwidth supporting rapid OEM re-orders and multi-tier sports supply chains.
Strict production milestone monitoring ensuring international brands hit critical seasonal shelf dates.
China Factory 4.0: Supply Chain Resilience & Lean Scale Advantages
Headquartered in Sichuan, Sichuan MiFo Technology Co., Ltd. and Chengdu MiFo Biological Technology Co., Ltd. leverage advanced Italian computerized knitting units, zero-defect optical vision sorting, and direct clean hydropower sourcing.
Automated 168N–200N Lonati Platforms
Precision alpine hosiery requires micro-loop density that standard machines cannot knit. Our manufacturing floor features computerized single and double cylinder Lonati machines capable of continuous multi-feed Jacquard, variable compression dial controls, and automated closed-toe linking (Rosso-free toe seams), eliminating chafing points over metatarsal regions.
Sichuan Clean Hydropower & Low-Carbon Base
Situated in Western China's renewable energy corridor, our 42,000 m² campus operates with a high ratio of clean hydroelectric power. This foundational energetic advantage substantially reduces Scope 2 greenhouse gas emissions per dozen pairs produced, enabling our international partners to seamlessly pass EU carbon boundary adjustments and ESG audits.
MES-Driven Real-Time Quality Control
Every knitting station connects to a central Manufacturing Execution System (MES). Optical yarn-break sensors, in-line tension strain gauges, and automated digital pairing ensure stitch consistency across 100,000+ unit production lots. Defect deviations trigger immediate needle stops, maintaining downstream scrap rates under 0.6%.
Macro Industry Solutions: Sourcing Protocols by Application
From extreme Alpine World Cup competition to family resort rentals, trampoline entertainment centers, and medical slipper programs: here is how global sourcing leaders specify their yarn and knitting matrices.
| Hosiery Category | Architectural Construction | Engineered Fiber Matrix | Branding & Finishing Customization | Primary Industrial Sector |
|---|---|---|---|---|
| Pro World Cup Ski Socks | Ultra-thin 200N needle density, zero-cushion footbed, high-friction heel pocket, graduated compression (18-22 mmHg). | 52% Merino Wool (17.5μm), 38% Polyamide 6.6, 10% Lycra elastane. | 360° micro-jacquard graphics, high-definition cuff brand tags, silicone arch lockdown bands. | Performance Alpine Brands, National Ski Teams, Pro Ski Shops. |
| All-Mountain & Backcountry Socks | 3D anatomical terry padding on shin, Achilles tendon, and sole; ventilation vapor mesh along instep; seamless linking. | 65% Merino Wool, 25% Cordura Nylon, 8% Polyester, 2% Spandex. | Reflective yarn inserts, heat-transfer size labeling, eco-friendly FSC kraft paper retail sleeves. | Outdoor Retail Chains, Ski Resort Concessions, Alpine Rental Fleets. |
| Trampoline & Commercial Grip Socks | High-traction silicone grip patterns on full sole, reinforced elastic arch wrap, high-rebound terry cushion footbed. | 80% Combed Cotton, 17% Polyester, 3% Spandex with Food-Grade Non-Toxic Silicone. | Custom molded silicone grip logos, size-specific color heel rings, individual polybag barcodes. | Trampoline Parks, Indoor Play Arenas, Yoga & Pilates Franchises. |
| Aqua Park & Watersport Socks | Quick-dry hydrophobic textile, micro-perforated water-draining sole, continuous abrasion-resistant rubberized grip. | 85% Fast-Dry Polyester, 15% Elastane with Chlorinated-Water Resistant Additives. | Sublimated all-over branding, high-visibility neon safety cuffs, retail hanger packaging. | Commercial Waterparks, Surf Schools, Thermal Spring Resorts. |
| Hospital Patient Slipper Socks | Double-sided anti-fall traction tread, non-constricting non-elastic top band, plush terry lining for sensitive skin. | 88% Virgin Acrylic / Cotton Blend, 10% Polyester, 2% Conductive Antistatic Fiber. | Clinical color risk coding (Red/Yellow/Green), facility thermal transfer logos, bulk carton packing. | Healthcare Networks, Elder Care Facilities, Orthopedic Clinics. |
| High-Performance Sports Socks | Hexagonal arch compression band, Achilles blister shield, anti-odor silver ion treatment, high-durability heel/toe reinforcement. | 60% Cotton, 30% Polyamide, 10% Spandex with Ionic+ antimicrobial silver yarn. | Team crest intarsia knitting, personalized player numbering, presentation gift boxes. | Football / Basketball Clubs, Cycling Teams, Athletic Footwear Brands. |
Technical Roadmap & Future Outlook: Next-Gen Ski Sock Tech
Discover how our research laboratory in Chengdu is pushing the technological boundaries of wearable thermal textiles, smart heating integration, and circular closed-loop synthetics through 2028.
Phase-Change Materials (PCM) & Micro-Encapsulated Thermoregulation
Traditional ski socks rely solely on static trapping of air. Our upcoming engineering cycle introduces paraffin-based micro-encapsulated PCM fibers directly into the tibial and toe box areas. These fibers actively absorb excess thermal energy during vigorous mogul or downhill runs and release stored heat when waiting on freezing chairlifts, maintaining skin boundary temperatures at a constant 31°C–33°C.
Knitted Conductive Polymer Pathways for Ultra-Thin Heated Socks
Eliminating bulky carbon wire inserts: our R&D team has prototyped seamless intarsia knitting using silver-coated polyamide micro-filaments. These conductive pathways form an imperceptible, flexible heating zone beneath the toe box, powered by miniaturized 3.7V / 5V lithium pack connections at the welt. The result is a high-performance race-fit heated ski sock with zero boot pressure points.
Bio-Synthetic Polyamides & Recycled Polymer Circularity
Meeting the stringent European Green Deal and PEF (Product Environmental Footprint) targets, we are transitioning nylon contents to 100% post-consumer discarded fishing nets (Econyl/rPA6) and bio-based polyamides synthesized from non-food castor bean oil. Combined with Chlorine-Free certified washable Merino wool, our 2026+ ski socks achieve a 48% reduction in lifecycle CO₂ footprint.
Global Compliance, Rigorous Testing & Ethical Governance
We eliminate commercial risk for Fortune 500 sports conglomerates and boutique labels through exhaustive chemical analysis, fair labor verification, and certified trade documentation.
OEKO-TEX Standard 100
Every single yarn batch, elastane thread, dye formulation, and silicon grip compound is tested against 300+ regulated substances, certified completely free of hazardous amines, PFAs, and toxic plasticizers.
BSCI & Sedex Audited
Our Sichuan industrial facilities maintain strict compliance with SMETA four-pillar social audits and BSCI standards: fair compensation, zero child labor, rigorous occupational safety, and equitable labor governance.
US Prop 65 & REACH
Strict heavy-metal limits, zero banned phthalate plasticizers in silicone grips, and full documentation compliance for hassle-free North American Customs clearance and European chemical safety registration.
Mulesing-Free Wool Tracking
We source raw merino fibers exclusively from certified non-mulesed farms across Australia and South America, with complete chain-of-custody documentation and Responsible Wool Standard (RWS) traceability.
How Global Brands Scale Custom Production Programs
From initial tech pack hand-off to retail-ready distribution, our structured five-stage engineering process ensures uncompromising quality, brand fidelity, and supply chain predictability.
1. Technical Proofing
Our hosiery CAD engineers convert your sketches, vector artwork, or physical reference samples into pixel-exact machine needle charts, confirming stitch tensions, fiber ratios, and compression gradients within 48 hours.
2. Rapid Lab Prototyping
Using stock technical yarns and in-house computerized sample machines, we produce prototype pairs within 5–7 working days, complete with lab-certified elongation and compression test reports for fit testing.
3. Automated Bulk Runs
Upon sample approval, high-speed automated knitting lines run with continuous inline optical inspection. Multi-zone terry knitting, silicone grip vulcanization, and heat-boarding finalize hand-feel and dimensional stability.
4. Custom Packaging & DDP
Retail-ready presentation: FSC-certified paper bands, hangtags, custom polybags, or embossed gift boxes with UPC barcodes. We coordinate complete sea, air, or rail freight with DDP terms directly to your regional warehouse.
Frequently Asked Technical & Commercial Questions
Straightforward answers from our engineering directors regarding yarn choices, machine gauges, minimum orders, and supply chain timelines.
For competition-level race fit and backcountry touring, 168-needle and 200-needle single-cylinder machines with terry capability are optimal. They allow dense, low-bulk knitting that transfers kinetic micro-movements to ski boot shells instantly. For high-volume thermal resort socks, 144N or 132N heavy-gauge loops offer maximized trapped air loft for casual recreational skiers.
We employ a core-spun yarn architecture: fine-micron Australian Merino wool (18.5μm) is wrapped around a high-tenacity nylon or elastane filament core. The exterior provides pure wool thermal regulation and odor resistance against the skin, while the synthetic interior core prevents heel friction abrasion, blowouts, and shrinking during machine laundering.
For fully customized technical ski socks utilizing custom-dyed Pantone yarns, our standard baseline MOQ is 1,200 pairs per colorway/size split. For stock yarn programs, we accommodate agile runs starting at 500 pairs. Rapid technical prototypes are developed and dispatched via DHL within 5–7 business days of CAD pattern confirmation.
Yes. Using advanced computerized elastane tension feeds on our Italian Lonati platforms, we knit true graduated compression following European RAL-GZ 387 and ISO 13485 standards. Pressure profiles are highest at the ankle (Class 1: 15–20 mmHg or Class 2: 20–30 mmHg) and systematically decrease toward the proximal calf to enhance venous return during rigorous descents.
We are a direct manufacturer. Founded in 2013, our production campus spans 42,000 square meters in Sichuan, China, housing over 500 automated knitting machines, in-house finishing lines, silicone screen printing workshops, and an annual production capacity surpassing 200 million pairs of specialized socks for international retail brands.
We offer complete turnkey retail packaging: FSC-certified paper carding, bio-based biodegradable polybags, woven labels, and retail shelf display cartons printed with soy inks. All materials comply with the latest EU Packaging and Packaging Waste Regulation (PPWR) and US state environmental packaging mandates.
Expanded Specialty & Multi-Category Collections
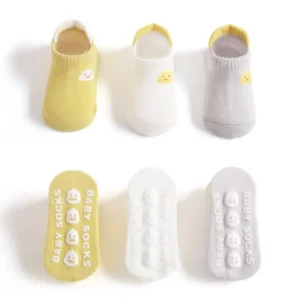
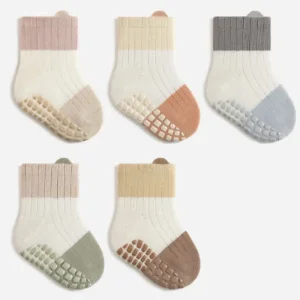
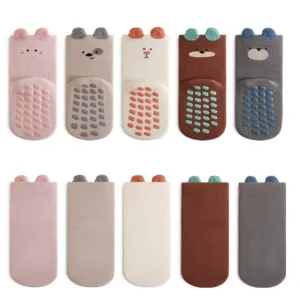
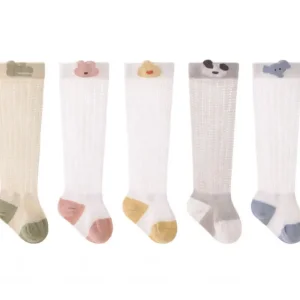
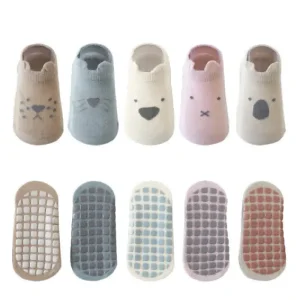
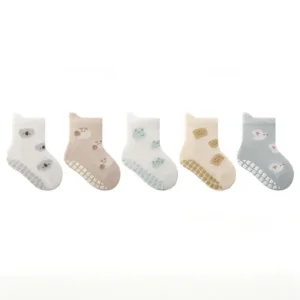
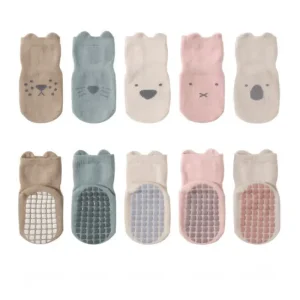
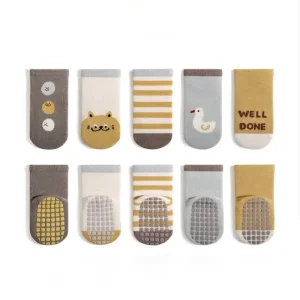
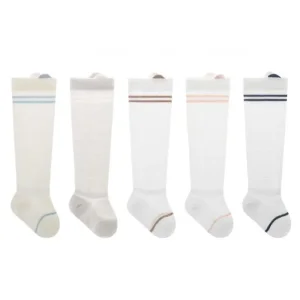
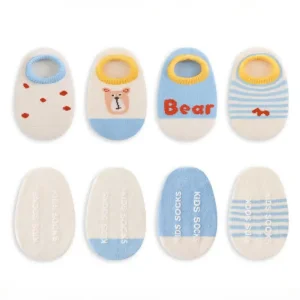
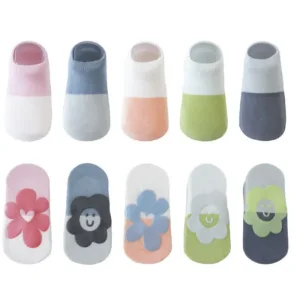
Explore additional specialized hosiery lines engineered for anti-slip safety, summer ventilation, high-impact playground friction, and protective toddler support.
Ready to Engineer Your Next-Gen Alpine Sock Line?
Contact our Sichuan manufacturing headquarters directly. Our hosiery technical team reviews CAD designs, provides yarn composition suggestions, and supplies sample estimates within 24 business hours.