Enterprise Sample Showcase (Part 1)
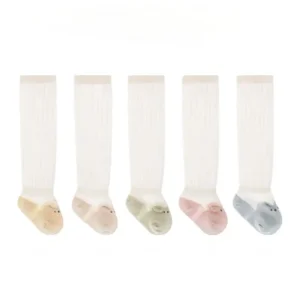
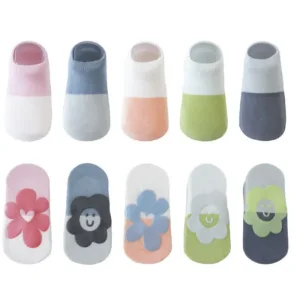
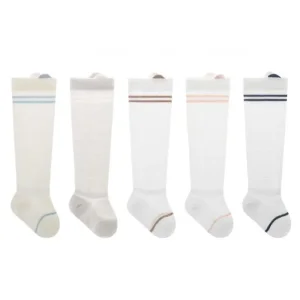
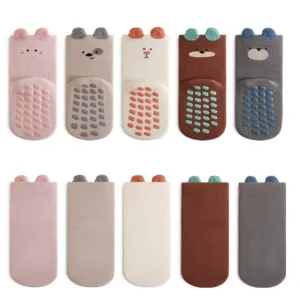
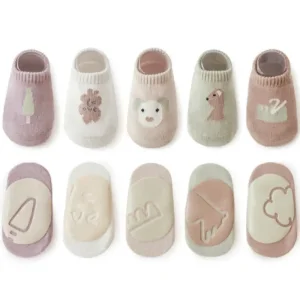
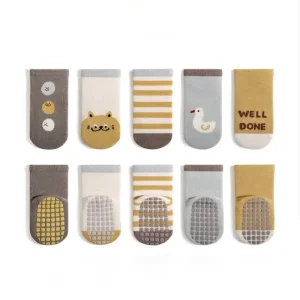
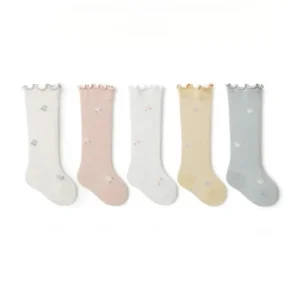
Direct factory catalog highlighting specialized non-slip technology, cooling fibers, and ergonomic infant-to-adult transitional hosiery specifications.
Executive Overview: Modern Textile Engineering in Men's Sock Manufacturing
Shift from commodity hosiery to precision-engineered apparel: How modern yarn science and computerized knitting drive higher margins and brand equity.
In today's global market, men's socks are no longer viewed merely as functional basics. They represent an essential intersection of ergonomic support, thermal management, bio-mechanical stability, and high-margin retail positioning. Global buyers, brand directors, and procurement executives require suppliers capable of executing complex tech packs with absolute consistency across high-volume production runs.
As a premier OEM/ODM manufacturer, our China-based industrial facility integrates end-to-end production—from raw yarn texturing and computerized 144N, 168N, and 200N Lonati knitting to automatic seamless toe linking, silicone grip application, boarding, and customized retail packaging. By combining high-grade combed cotton, silver-ion antibacterial filaments, CoolMax moisture-transport fibers, and GRS-certified recycled polyester, we deliver hosiery solutions that achieve unparalleled comfort and structural longevity.
Strategic Supply Chain Advantages: China's Integrated Hosiery Ecosystem
Why leading global retailers source men's and specialized functional hosiery from China's advanced manufacturing clusters.
Upstream Raw Material Integration
Direct proximity to world-class yarn spinning mills provides priority access to premium combed cotton, mercerized long-staple cotton, bamboo viscose, and technical synthetic filaments at locked-in cost efficiencies.
Automated Italian Knitting Machinery
Utilizing high-speed, fully computerized Lonati and Santoni knitting machinery guarantees zero-defect stitch geometry, precise tension control, multi-color jacquard intricacy, and seamless toe-closing functionality.
Agile Prototyping & Rapid Scale
3D CAD patterning and digital knitting enable sample development within 3 to 5 business days. Scalable floor space allows seamless expansion from 1,000-pair trial orders to multi-million pair seasonal rollouts.
Technical Engineering & Sourcing Specifications Matrix
Detailed comparative matrix designed for procurement teams, technical designers, and QA directors defining product lines.
| Sock Category | Needle Gauge / Count | Core Fiber Composition | Structural Features | Target B2B Application |
|---|---|---|---|---|
| Executive Business Dress | 200N Ultra-Fine | 80% Mercerized Combed Cotton, 17% Nylon, 3% Spandex | Extended cuff elasticity, hand-linked seamless toe, subtle luster finish | Luxury Retail, Corporate Uniforms, Direct-to-Consumer Brands |
| Athletic & Performance Grip | 168N / 144N Terry | 65% CoolMax Polyester, 25% Cotton, 10% Elastane | 3D arch compression band, targeted heel/toe terry padding, silicone traction sole | Professional Sports Clubs, Trampoline Parks, Gym Accessories |
| Heavy-Duty Tactical / Workwear | 144N Double Cylinder | 50% Wool / Acrylic, 35% Cordura Nylon, 15% Elastane | Reinforced Kevlar heel pocket, high thermal rating, anti-friction sole cushion | Industrial Safety Supply, Military Gear, Outdoor Equipment Retailers |
| Medical & Non-Binding Diabetic | 168N Smooth Knit | 75% Organic Bamboo Viscose, 20% Nylon, 5% Lycra | Non-binding top cuff, cross-stretch calves, silver-ion antibacterial treatment | Healthcare Distributors, Pharmacies, Senior Living Care Centers |
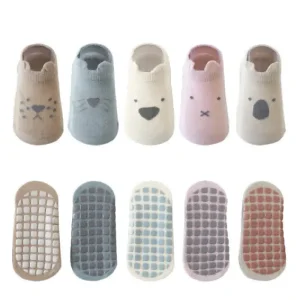
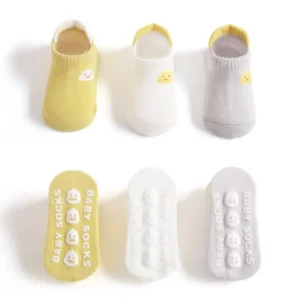
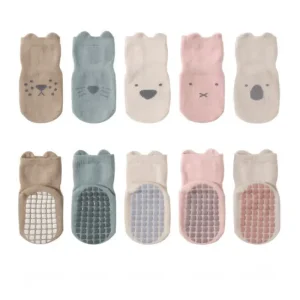
| Infant & Toddler Grip Series | 144N Soft-Knit | 82% Combed Organic Cotton, 15% Nylon, 3% Spandex | Eco-friendly non-slip silicone tread, OEKO-TEX Class 1 safe dyes, turn-cuff design | Baby Boutique Networks, Mass Retail Department Stores |
Localization Support, Compliance & Regulatory Assurance
Navigating international trade hurdles with comprehensive certification frameworks and localized market adaptations.
Global Certification Standards
Our manufacturing operations are fully compliant with OEKO-TEX Standard 100 (Class 1 & 2), BSCI social audits, Sedex SMETA, and GRS (Global Recycled Standard), facilitating smooth import clearances into European, North American, and Asia-Pacific markets.
Chemical & Safety Compliance
Every yarn batch undergoes rigorous testing for AZO dyes, phthalates, formaldehyde, and heavy metals in accordance with EU REACH regulations and US CPSC/CPSIA requirements, guaranteeing skin safety and hypoallergenic properties.
Localized Door-to-Door Logistics
We provide comprehensive DDP (Delivered Duty Paid), FOB, and CIF logistics packages. Our export department handles customs clearance, localized barcode labeling, FSC packaging compliance, and warehousing integration.
Industry Trends & Future Hosiery Innovations (2025–2030)
Emerging technologies shaping the global sock manufacturing landscape: From bio-based polymer yarns to custom-printed silicone traction structures.
1. Eco-Conscious Materials and Circular Textiles
Sustainability is no longer an optional marketing angle; it is a baseline procurement prerequisite. Major retail groups are replacing virgin synthetic fibers with recycled post-consumer PET bottles (RPET) and organic natural plant fibers. Innovations like micro-modal sourced from sustainable beechwood and recycled cotton yarn reduce water consumption during dyeing by over 40% while delivering incredible softness.
2. Biomechanical & Targeted Ergonomic Knitting
Modern men's dress and sports socks incorporate advanced anatomical mapping. Left/Right foot asymmetrical knitting ensures optimal toe box alignment, preventing friction blisters. Zone compression around the plantar fascia and ankle tendon improves blood circulation and reduces fatigue for active professionals and endurance athletes alike.
3. Specialized Anti-Slip and Hospital Safety Innovations
Custom silicone grip application has evolved from simple dots to intricate geometric traction networks. Using food-grade, non-toxic silicone compounds, heat-cured directly onto high-density knit soles, our grips deliver slip resistance across wet tile, polished hardwood, trampoline canvas, and hospital linoleum surfaces.
Localized Application Scenarios & Market Deployment
How our customized hosiery configurations adapt to specialized commercial environments and end-user lifestyles.
Corporate & Executive
200-needle fine-gauge cotton dress socks designed for formal business attire. Anti-microbial treatments keep feet fresh during long working hours and transcontinental flights.
Sports & Athletics
High-cushion football, basketball, and running socks featuring channel ventilation, arch support, and anti-blister yarn construction for maximum athletic output.
Indoor Parks & Yoga
Custom-branded grip socks designed for trampoline facilities, indoor playgrounds, pilates, and aqua parks, prioritizing sanitary protection and slip safety.
Infant & Family Lines
Soft-touch, non-irritating newborn, infant, and child socks featuring anti-mosquito weaves, organic cotton blends, and gentle non-binding cuffs.
Enterprise Sample Showcase (Part 2)
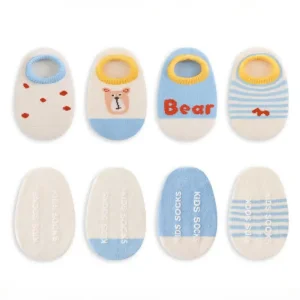
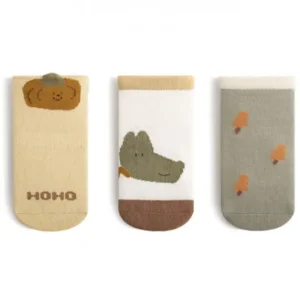
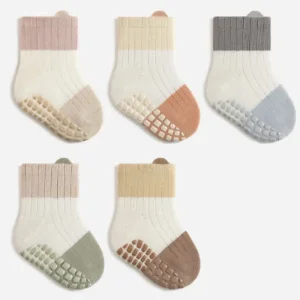
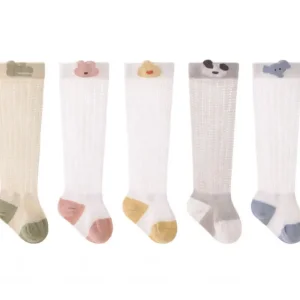
Explore additional specialized lines including colorful infant ankle socks, long-tube breathable knits, and premium non-slip toddler hosiery.
Enterprise Procurement FAQ (Frequently Asked Questions)
Direct answers from our engineering and international trade department addressing B2B client concerns.
What is your standard Minimum Order Quantity (MOQ) for custom men's socks?
Our standard Minimum Order Quantity (MOQ) is typically 1,000 to 3,000 pairs per design/colorway depending on yarn complexity and needle specification (e.g., 200N vs 144N). For stock colors and standard combed cotton yarns, lower trial order quantities can be negotiated to support market testing.
Can you manufacture custom silicone grip designs with our brand logo?
Yes, absolutely. We specialize in custom silicone traction application. We can translate your brand logo, icon, or custom non-slip pattern into high-durability silicone soles using heat-curing screen printing technology. The silicone is non-toxic, eco-friendly, and engineered to withstand 50+ industrial wash cycles without peeling.
What certifications do your factory and raw materials carry?
Our manufacturing plant undergoes regular social compliance audits including BSCI and Sedex SMETA. All raw yarn blends carry OEKO-TEX Standard 100 certification, assuring compliance with strict international chemical safety standards, REACH (EU), and CPSC (USA) testing criteria.
What is the turn-around time for sampling and mass production?
Digital technical proofs are completed within 24 hours. Physical pre-production samples require 3 to 7 business days. Once samples are approved, standard mass production lead times range between 20 to 35 calendar days depending on seasonal order volume and customized packaging requirements.
Do you offer private label packaging and custom retail headers?
Yes. We offer complete OEM/ODM private labeling services, including printed header cards, wrap bands, belly bands, custom box sets, FSC-certified recycled paper tags, barcode application, and retail display cartons ready for immediate distribution.
How do you ensure color consistency and quality control across large orders?
We strictly implement Pantone (TCX/TPX) color matching protocol with spectrophotometer verification. Quality control follows AQL 1.5 / 2.5 standards across four inspection stages: raw yarn tension test, in-line knitting check, post-linking/boarding verification, and final carton packing audit.