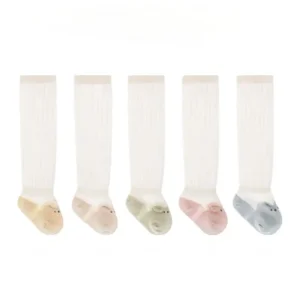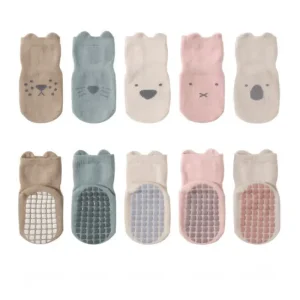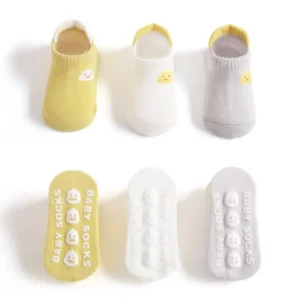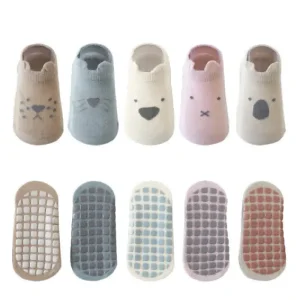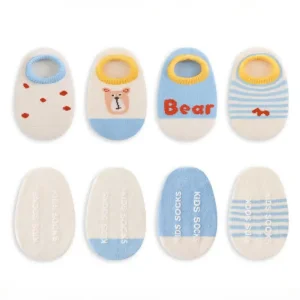
Catalog Showcase: Pediatric & Anti-Slip Clinical Series
Direct manufacturing specs: high-elastic retention, skin-safe biocompatible yarns, and durable thermoset non-slip matrices engineered for heavy-cycle machine washing.
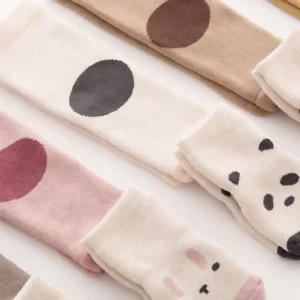
Evolution of Machine-Washable Medical Socks
The global healthcare textile industry is pivoting from disposable PPE toward sustainable, multi-cycle reusable hosiery engineered for rigorous institutional infection-control standards.
Reusable Circular Economy
Global hospital networks are reducing single-use waste. Modern washable medical socks withstand 50+ commercial washing cycles at 60°C–90°C thermal sanitization conditions without elasticity degradation or grip detachment.
Clinical Fall Prevention Protocols
Patient falls account for significant healthcare liabilities. Machine-washable socks feature high-friction thermoset silicone patterns strategically formulated for wet institutional vinyl, terrazzo, and tile surfaces.
Biocompatible Fiber Matrices
Certified OEKO-TEX® combed cotton and synthetic microfibers blended with non-migrating antimicrobial agents eliminate bacterial colonization while staying fully hypoallergenic on fragile geriatric or pediatric skin.
Enterprise Sourcing: Navigating Compliance & Total Cost of Ownership
B2B hospital supply directors and healthcare distributors balance upfront production economics against durability, safety certifications, and supply chain consistency.
Total Cost of Ownership (TCO)
Procuring durable washable socks reduces annualized textile spend by up to 40% compared to purchasing single-use variants repeatedly, despite minor increases in per-unit manufacturing costs.
Social & Regulatory Audits
Institutional contracts mandate verified production facilities. Our manufacturing lines carry full BSCI and Sedex compliance, ensuring end-to-end traceability, worker safety, and ethical labor standards.
Color-Coded Triage Protocols
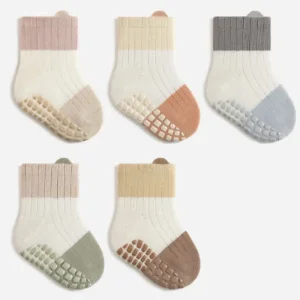
Enterprises require strict color indexing (e.g., Red for High Fall Risk, Yellow for Allergy Precaution, Green for Universal). Factory-direct dying delivers consistent colorfastness resistant to heavy industrial bleach.
China Factory 4.0: Supply Chain Resilience & Efficiency
Combining Sichuan MiFo Technology's automated 42,000 m² smart infrastructure with lean supply logistics, delivering exceptional reliability for high-volume healthcare programs.
Automated Precision Knitting
Computerized circular knitting units calibrate tension across the welt, instep, and sole, eliminating abrasive toe seams and ensuring uniform graduated compression profiles across millions of units.
Thermal Silicone Vulcanization
Our proprietary silicone bonding process vulcanizes polymer tread designs directly into the yarn structure under controlled heat and pressure, preventing grip peel-off during high-temperature laundry cycles.
Multi-Stage Inline QA
Every lot passes comprehensive yarn tensile testing, wash-shrinkage verification, grip-friction coefficient benchmarking (ASTM standards), and final metal detection before packaging.
Localized Applications & Use-Case Profiles
Medical-grade machine-washable hosiery adapts to distinct operational environments across global clinical and rehabilitation facilities.
| Facility Type | Core Functional Focus | Yarn Specification | Grip Geometry & Placement | Compliance Mandate |
|---|---|---|---|---|
| Acute Care Hospitals | Rapid Fall Risk ID & Hygiene | Poly-Cotton + Covered Spandex | Double-sided (360°) dot matrix | EN ISO Sanitization, Non-Binding |
| Long-Term Eldercare | Edema Relief & Shear Reduction | Combed Organic Cotton blend | Full-sole contoured chevron tread | BSCI, OEKO-TEX Standard 100 |
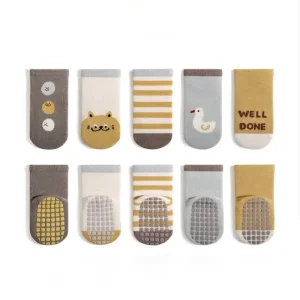
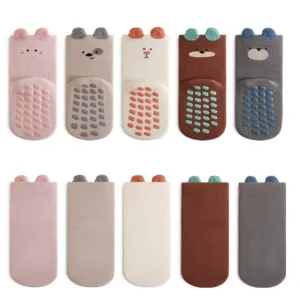
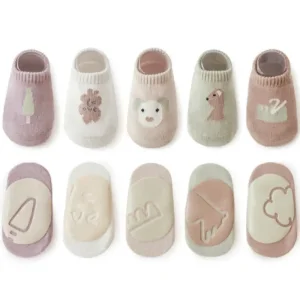
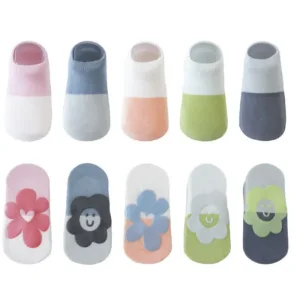
| Pediatric Inpatient | Skin Safety & Non-Constrictive | Hypoallergenic Cotton + Lycra | Fun customized animal/geometric grip | CPSIA, REACH Compliant non-toxic |
| Rehab & Physical Therapy | Gait Stability & Proprioception | Technical Nylon-Spandex blend | Segmented anatomical flex-zones | High-friction ASTM Dynamic CoF |
Expert Guidance on Custom Medical Socks Manufacturing
Direct answers from our engineering and export departments addressing durability, certification, minimum orders, and customization.
What makes medical socks truly "machine-washable" compared to promotional socks?
Can you produce double-sided grip socks for disoriented or elderly patients?
What are the Minimum Order Quantities (MOQs) for custom colors and logo silicone treads?
Are materials compliant with US and European healthcare standards?
How does Sichuan MiFo ensure supply chain consistency for recurring container orders?
High-Performance Pediatric & Anti-Slip Clinical Solutions
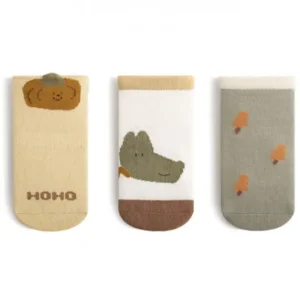
Explore our export-ready sock inventory engineered for clinical hygiene, specialized comfort, and commercial durability.