Direct Manufacturing Portfolio
High-Performance Custom Golf & Specialty Socks
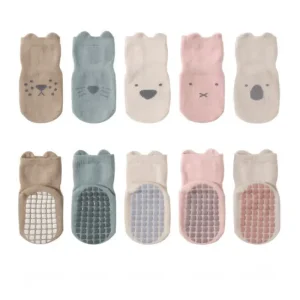
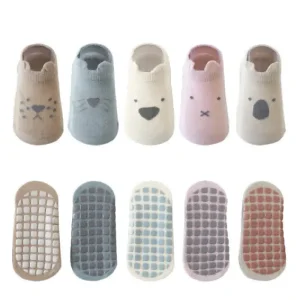
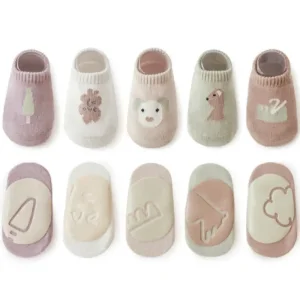
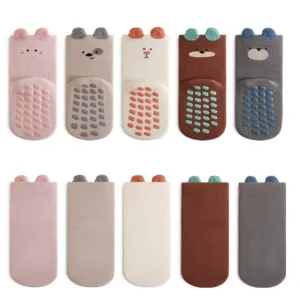
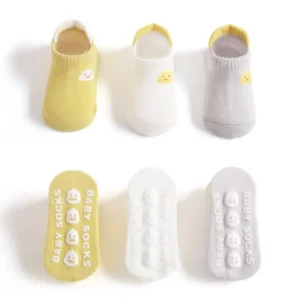
Explore our certified baseline designs engineered with anti-slip silicone, reinforced micro-cushioning, and precision needle configurations for international supply contracts.
Enterprise Procurement Framework
Corporate Sourcing Requirements in the Performance Golfing Sector
Modern golf apparel buyers require strict technical compliance, sustainable fiber tracing, and dynamic mechanical engineering rather than simple aesthetic branding.
200M+
Annual Unit Output
100+
Export Destined Nations
99.4%
On-Time Logistics SLA
42,000m²
Automated Smart Campus
Tier-1 Private Label Brands
Global golf athletic brands demand needle count precision (168N to 200N), targeted compression zones (15-20 mmHg at the plantar fascia), and anti-shearing yarn structures that minimize blister formation during an 18-hole round over 7 kilometers of varied terrain.
PGA Tournaments & Pro Shops
Resort-level pro merchandise programs prioritize ultra-fine combed cotton (40s/2 combed), mercerized Scottish lisle blends, high-definition 360° seamless jacquard club cresting, and presentation packaging meeting premium country-club retail standards.
Institutional & Corporate Golf Outings
Large corporate gifting entities prioritize low minimum run variance, rapid digital proofing (under 24 hours), automated multi-pack barcoding, and rapid transit guarantees that link manufacturing batch runs directly with fixed tournament timelines.
OEM/ODM Engineering
Macro-Industry Technical Solutions & Architecture
A structured breakdown of modern robotic hosiery manufacturing: converting raw bio-polymer pellets and combed fibers into specialized kinetic footwear accessories.
| Functional Zone | Structural Engineering Specification | Technical Fiber Selection | Biomechanical Performance Benefit |
|---|---|---|---|
| Plantar Arch Archway | Dual-band ribbed elastic knit (spandex cross-weave) | Lycra® T9026 with high-recovery filament core | Prevents mid-foot tendon fatigue and preserves arch elasticity through dynamic torque swing mechanics. |
| Heel & Achille Apex | Extended Y-heel pocket with French terry loop density | High-tenacity Polyamide 6.6 with air-jet texturing | Locks sock to foot anatomy; eliminates slippage inside spiked shoes during centrifugal hip turns. |
| Metatarsal Cushion | Selective loop density padding (0.8mm to 1.6mm loft) | Coolmax® moisture-transport hollow poly core | Absorbs downward swing strike impacts and ground reaction forces during prolonged fairway walks. |
| Dorsal Vent Channel | Open micro-mesh diamond jacquard architecture | Micro-denier recycled polyester (0.5 to 0.8 DPF) | Accelerates heat exchange and sweat vaporization, keeping feet cooler inside water-resistant leather footwear. |
| Non-Binding Cuff | Progressive soft-stretch ribbed collar | Elastane bare-spun double-covered yarn | Secures cuff placement without restricting vascular blood return or leaving circumferential indentations. |
R&D Trajectory
Technology Roadmap & Smart Hosiery Horizons (2025–2030)
Pioneering functional sports innovation through embedded sensory matrices, biomimetic cooling technologies, and carbon-negative closed loops.
Conductive Micro-Sensors & IoT
Development of flexible, wash-durable silver-coated yarn arrays integrated into the plantar sole to calculate ground-force reaction metrics, center-of-gravity shifts, and swing tempo data transmission directly to cloud analytics.
Phase-Change Thermodynamic Polymers
Infusing microscopic paraffin microcapsules directly into core synthetic filaments. When the foot experiences elevated skin temperatures above 32°C, the matrix absorbs latent heat, keeping microclimates dry and stable in summer rounds.
Closed-Loop Bio-Circular Synthetics
Switching bulk synthetic demand toward 100% post-industrial recycled PA6 (Econyl® compatible) alongside bio-fermented polyamides derived from industrial plant waste, slashing product embedded carbon footprints by up to 68%.
Industrial Operations
Global Supply Chain Realities: Nearshoring vs. Concentrated Manufacturing
Strategic analysis of cost dynamics, raw material integration, and high-speed robotic knitting floor capabilities across world regions.
Vertical Integration
China continues to command unprecedented advantages in technical hosiery due to localized upstream synthesis—from spinning, dyeing, and spinning core covers to computerized circular knitting machines (e.g., Lonati, Sangiacomo) within tightly integrated geographic clusters.
Nearshoring Trade-Offs
While European (Portugal, Italy, Turkey) and Central American (CAFTA-DR) hubs offer shorter sea transit to US and EU distribution channels, they experience 40–70% higher per-unit conversion costs and limited specialized yarn availability for intricate athletic compression runs.
Logistics Predictability
Our centralized 42,000 m² Sichuan facility hedges export vulnerability through multiple rail corridors into Europe (China-Europe Railway Express) alongside high-capacity direct ocean links via Shenzhen and Shanghai to the Americas and Oceania.
Agile MOQ Structuring
Balancing scale efficiency with customized capsule releases. Our high-throughput automated floors easily process high-volume seasonal inventory batches alongside responsive re-orders as low as 1,200 pairs per SKU.
Total Quality Assurance
International Regulatory Compliance & Testing Protocols
Ensuring complete chemical safety, mechanical strength, and ethical chain-of-custody verification for high-risk retail consumer environments.
OEKO-TEX® Standard 100 Class I & II
Every lot is verified free of banned azo colorants, nickel, lead, cadmium, chlorinated phenols, and harmful PFAS water-repellent coatings, ensuring absolute skin contact neutrality under hot, sweaty friction conditions.
BSCI & Sedex SMETA Audit Pillars
Uncompromising ethical compliance covering labor welfare, health and factory safety, living-wage metrics, environmental management systems, and transparent business ethics documentation available on demand.
ASTM / ISO Rigorous Laboratory Benchmarks
Certified in-house lab validation: Martindale Abrasion Test (ASTM D4966) passing 30,000+ rubs without filament pill breaks, colorfastness to artificial perspiration (ISO 105-E04) rated grade 4-5, and stretch-recovery cycles tested via Instron tensiometers.
Purchasing & Operations Q&A
Frequently Asked Procurement Questions
Comprehensive technical and commercial clarification for professional procurement leaders and brand managers.
What is the typical production lead time for custom golf socks?
Pre-production physical sampling takes 5–7 business days following technical CAD drawing approval. Bulk mass production requires 20–30 calendar days depending on yarn dyeing requirements, needle complexity, and custom packaging finishing specifications.
What needle counts do you deploy for athletic and golfing categories?
We primarily utilize 144N, 168N, and 200N single and double-cylinder computerized machines. For high-cushion tour socks, 144N or 168N provide optimal terry loop plushness, whereas 200N delivers ultra-dense, low-profile, dress-sport silhouettes with crisp jacquard resolution.
Can you manufacture customized non-slip silicone traction patterns?
Yes. We operate proprietary automated rotary and screen silicone application lines capable of molding custom logo geometries, directional chevron micro-dots, and varying shore-hardness compounds directly onto the exterior sock sole to increase internal shoe grip.
What are the minimum order quantities (MOQ) per design and colorway?
Standard minimums start at 1,200 pairs per style/colorway using in-stock combed cotton or technical synthetic yarn colors. Fully custom-dyed Pantone color match programs start at 3,000 pairs to satisfy minimum dye vat run requirements.
How do you accommodate private-label retail packaging requirements?
Our turnkey capabilities include FSC-certified recycled cardstock header cards, custom debossed slide-out gift drawer boxes, thermoformed transparent polybags, hangtags with integrated UPC/EAN barcodes, and retail point-of-sale display cartons ready for dispatch.
What trade Incoterms and shipping services do you offer?
We provide full EXW, FOB (Shanghai/Shenzhen), CIF, and end-to-end DDP (Delivered Duty Paid) shipping to private distribution centers across North America, Europe, Australia, and Asia via multimodal ocean, express air, and trans-Eurasian rail networks.
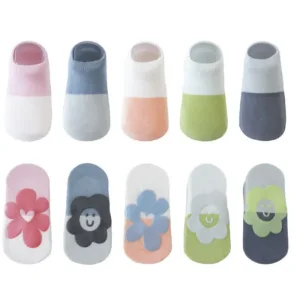
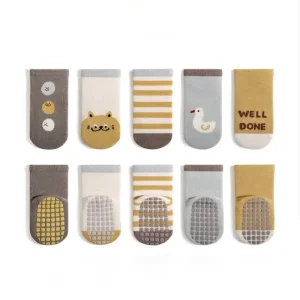
Specialty Knitwear & Grip Portfolio
Precision Anti-Slip, High-Tube & Performance Children's Lines
Demonstrating our specialized versatility across non-slip rubberized dots, infant skin ergonomics, and technical seamless finishing options.